Farabi At A Glance
Farabi At A Glance
Farabi Pharmaceutical company which was inaugurated in January 1993 for the mass production of antibiotics is the leading pharmaceutical company in the region.
The Complex enjoys a wealthy ten acre work space site built in a forty hectare stretch of land, itself advantageously placed on the higher grounds adjacent to the southern mountains of Isfahan.
The Complex produces various oral antibiotic-related and non-antibiotic products and dietary supplements which sets the prestigious annual production record of 1,200000,000 capsules 45,000,000 suspensions and 460,000,000 film-coated tablets .To guarantee the required clinical effect for its products, Farabi acquires its raw materials from the
most renowned and reliable international producers. All production procedures are managed
According to the cGMP guidelines, FDA and WHO, with the most up to date production machinery and equipment right from granulation down to packing and cartoning, based on the international standards EP, BP, USP. Furthermore Managerial regulatories such as:
Quality Management “ISO 9001:2008 “, Environment Management “ISO 14001:2004 “ and
Occupational Health System & Safety” OHSAS 18001:2007 “have been stabilized atfarabi by the MIC institute of England.. Also stabilized laboratory management “ISO 17025:2008” by the NACI center.
Farabi Pharmaceutical Company along with the growth and development of the pharmaceutical industry in the world has co-operated with several world major pharmaceutical companies such as:
GSK, SANDOZ, FUJISAWA, NOVELL, VALPHARMA and RANBAXY which has resulted in production of a number of Antibiotics such as Coamoxiclave and Cefixime and non- antibiotics such as FeFar (Iron Sulfate + Folic Acid) which is produced under license.
Stringent quality control, as well as excellent raw materials from these companies, has yielded very fine products for demanding patients.


Main Activity
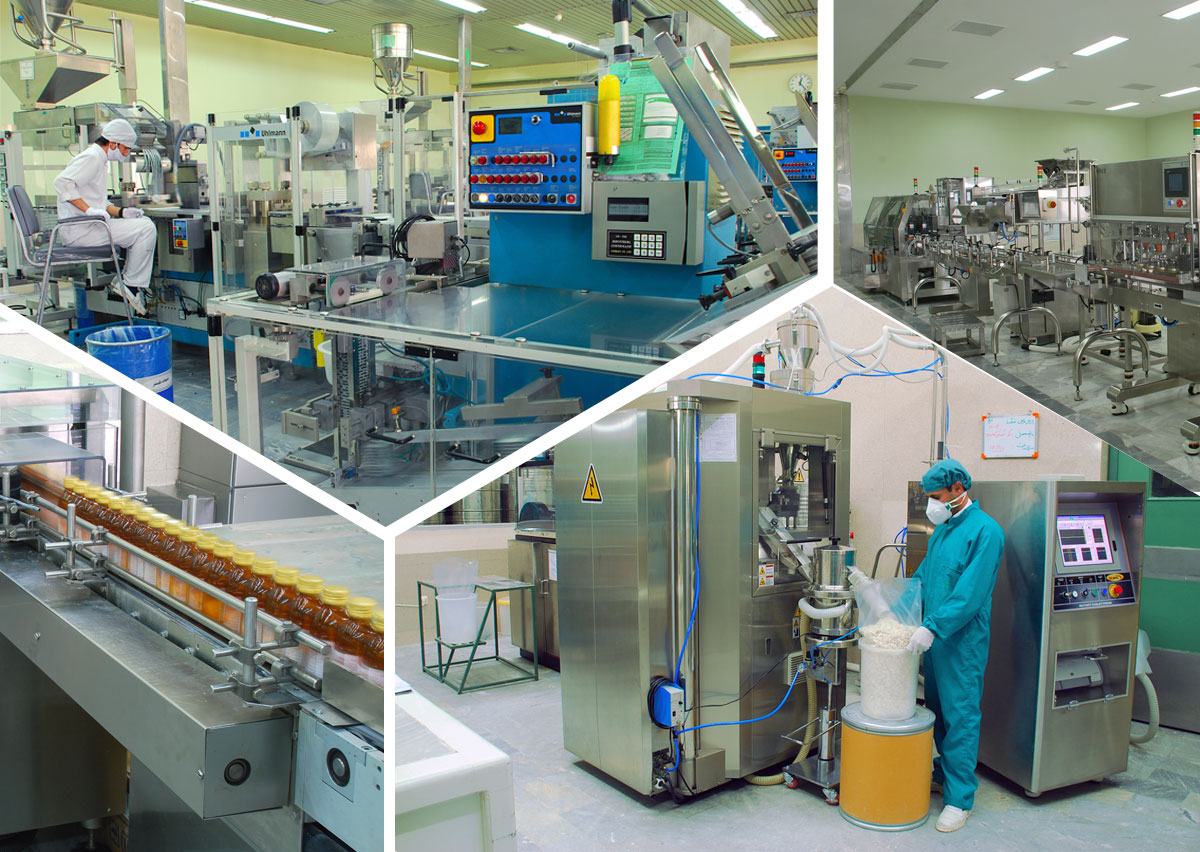
Since all pharmaceutical products aim at health recovery, three factors must be highlighted as crucial watch points during the manufacturing process: safety, bioavailability and stability.
To secure international standards in a pharmaceutical product, it is inevitable that the formulation, mixing, batch preparation , filling and packaging of all products be done automatically with no dependence on manual handling. Adopting the cGMP guidelines and watching the often-made managerial quote “BOX IN A BOX”, each Farabi manufacturing process has its own special space and corresponding production line. In this way, products are protected against any contamination which might occur as the result of a shared interior manufacturing space. Different sections thus defined and specified are equipped with their own air-filtering systems. Advanced machinery facilitates the automatic handling of raw materials through the subsequent processes of formulation, mixing, batch preparation, filling and packaging. Another highlight of Farabi’s technological competence is its capability to convert fine powder to compact powder. As we know, it is an advantage for providing the medical powder with good distribution of particle size, good flow and higher chemical and physical stability.
This method is very useful and profitable for those compounds that are not stable in humidity or those compounds that are susceptible to hydrolysis.
Finally, Farabi Pharmaceutical Complex has been designed for the 21st century.
FARABI EXISTS TO PROMOTE THE WELL-BEING OF SOCIETY.

The first duty for any pharmaceutical manufacturing company is to be sure of maximum safety of its patients and its drugs effectiveness. To reach this guaranteed quality for Farabi products, different on-site laboratories work together such that quality control is found to be stringent at every stage of manufacturing in Farabi Complex. These laboratories are staffed with highly trained personnel who enjoy the academic as well as the experimental expertise required for performing the often-complex evaluation analysis. Quality control is maintained at FarabiComplex by observing unanimously approved international standards as well as the latest guidelines set by FDA. These checks cover all manufacturing steps, starting from the very act of purchasing the raw materials down to the culminating phase of packaging, storage and distribution. All in all, Farabi’s research panel including pharmacists, chemists, microbiologists, engineers and technicians have one aim: QUALITY.
Meanwhile, the results of bioequivalency and bioavailability studies have proved that Farabi quality control team’s efforts have not gone to void, as Farabi Pharmaceutical Complex has been honored the business initiative directions Gold Star Award for Quality in 1997.

There is always the need to emphasize that all pharmaceutical manufacturing centers strive to Prolong human life and this by necessity obliges them not to pollute nature or threaten organic life. Farabi Pharmaceutical Complex cares about soil, air and water as the essences of life.
Hence, it is expectable that Farabi would design and develop its own water recycling system to treat all human and industrial waste water by implementing chemical and biological methods.
The result is of course favorable and prevents the polluted water from contaminating soil, air and underground water resources exterior to the production site. Consequently, the recycled water is used for watering the green area.
As for the air-filtering systems, Farabi observes the guidelines of cGMP regarding Roll-O-Maticand Electro Static filters to absorb particles in the air and to prevent the scattering of the antibiotic powder through the let-out air.
Farabi’s congeniality with nature and the environment has not only brought about product quality promotion but also attracted the favorable attention of Iranian Organization for the Preservation of Environment which named and nominated Farabi Pharmaceutical Complex as the winner of the prestigious titular certificate The Green Industry” of the year, in 1999.
The department of research and development in Farabi Pharmaceutical Complex brings the bright future for better medicine production The research carried out by expert researchers is informed by the most recent pharmacological and chemical finds which are pertinent to the medical sciences. Farabi’s advanced laboratories and sophisticated devices are the envy of any research Centre for this precise analysis results, of equal importance is the close cooperation with universities and academic centers which is a routine program in Farabi Pharmaceutical Complex, Planning and developing innovative medicinal formulations, improving new manufacturing procedures as well as methods for quality control and product analysis, carrying out bioavailability studies and assessing innovative drug delivery systems are the major functions of this department.